 EN
 English
 русский
 عربى
 中文简体

The handle cutout looks simple. Two holes in the sides for the hands. But the cutout is a stress point. The full crate is lifted by those two openings, and the weight pulls on the material around them. The mold has to form the cutout with the right radius and the right wall thickness around it, or the crate tears at the handle on the first heavy lift.
A plastic logistics crate mould factory that machines the handle cores clean and reinforces the surrounding wall produces a crate that survives being picked up loaded. A mold that cuts the handle opening too sharp, or leaves the wall too thin around it, produces a crate that fails in the warehouse.
The Base Has to Sit Flat
A crate that rocks on the pallet jams the conveyor and tips on the truck. The base is a large flat section, and it holds heat during cooling. If the mold cools the base unevenly, the base warps and the crate never sits right.
A plastic logistics crate mould factory that places the cooling channels to pull heat evenly from the base produces the crate that sits flat. This is a cooling design decision, not a material decision. The same resin will warp in one mold and stay flat in another.
The Ribs Carry the Load
A crate full of bottles can weigh twenty kilos or more. The walls have to hold that without bowing. The ribs, molded into the walls, provide the stiffness without adding wall thickness everywhere.
Too few ribs and the wall flexes. Too many and the mold gets complex and the cycle slows. A plastic logistics crate mould factory that designs the rib pattern against the actual load produces the crate that holds and still runs at the target cycle.
Here is what a plastic logistics crate mould factory needs to deliver:
- Handle cutouts with proper radius and wall thickness
- Base cooling that keeps the bottom flat
- Rib pattern designed against the load
- Stacking lugs and nesting taper in the cavity
- Material-specific shrink allowance
- Deep-core cooling for the cycle time
The Material and the Draw
Crates run on HDPE or polypropylene. HDPE is tough and takes impact. PP is stiffer and holds its shape. The resin sets the shrink, and the shrink sets the cavity dimensions. A plastic logistics crate mould factory that designs for the specific resin produces a crate at the right size.
The crate is a deep draw. The core has to be cooled from the inside, often with bubblers or baffles. A mould factory that gets the deep-core cooling right hits the cycle time. One that does not runs slow.
The Grower, the Bottler, and the Plant
The produce grower moves harvest from field to packhouse. The bottler moves bottles through the filling line. The industrial plant moves parts from supplier to assembly. Different loads, same crate. A plastic logistics crate mould factory that understands the load builds the crate for it.
The Crate That Tears at the Handle
The crate tears at the handle because the cutout radius was too sharp or the wall around it was too thin. The crate warps because the base cooling was uneven. The crate flexes because the ribs were too few. None of these are material problems. They are mold design problems, and they show up months after the mold was built.
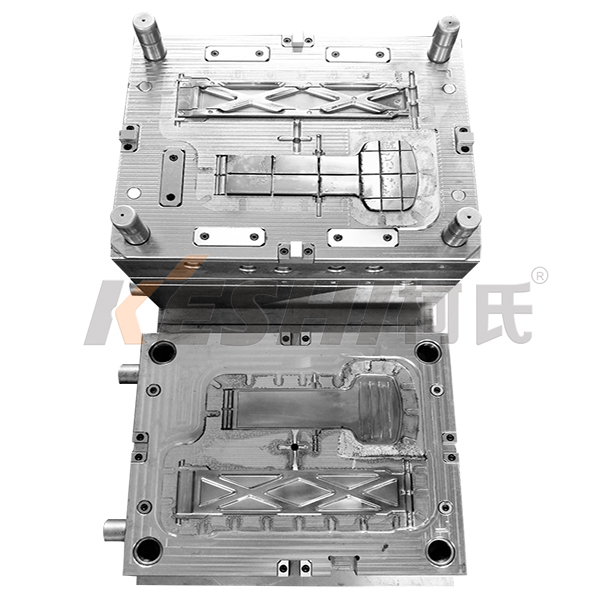
A plastic logistics crate mould factory builds the tooling behind the crate in the supply chain. The handle, the base, the ribs, the stack. Choose a factory that designs the load path, the cooling, and the rib structure. The crate will survive the warehouse.